Quality
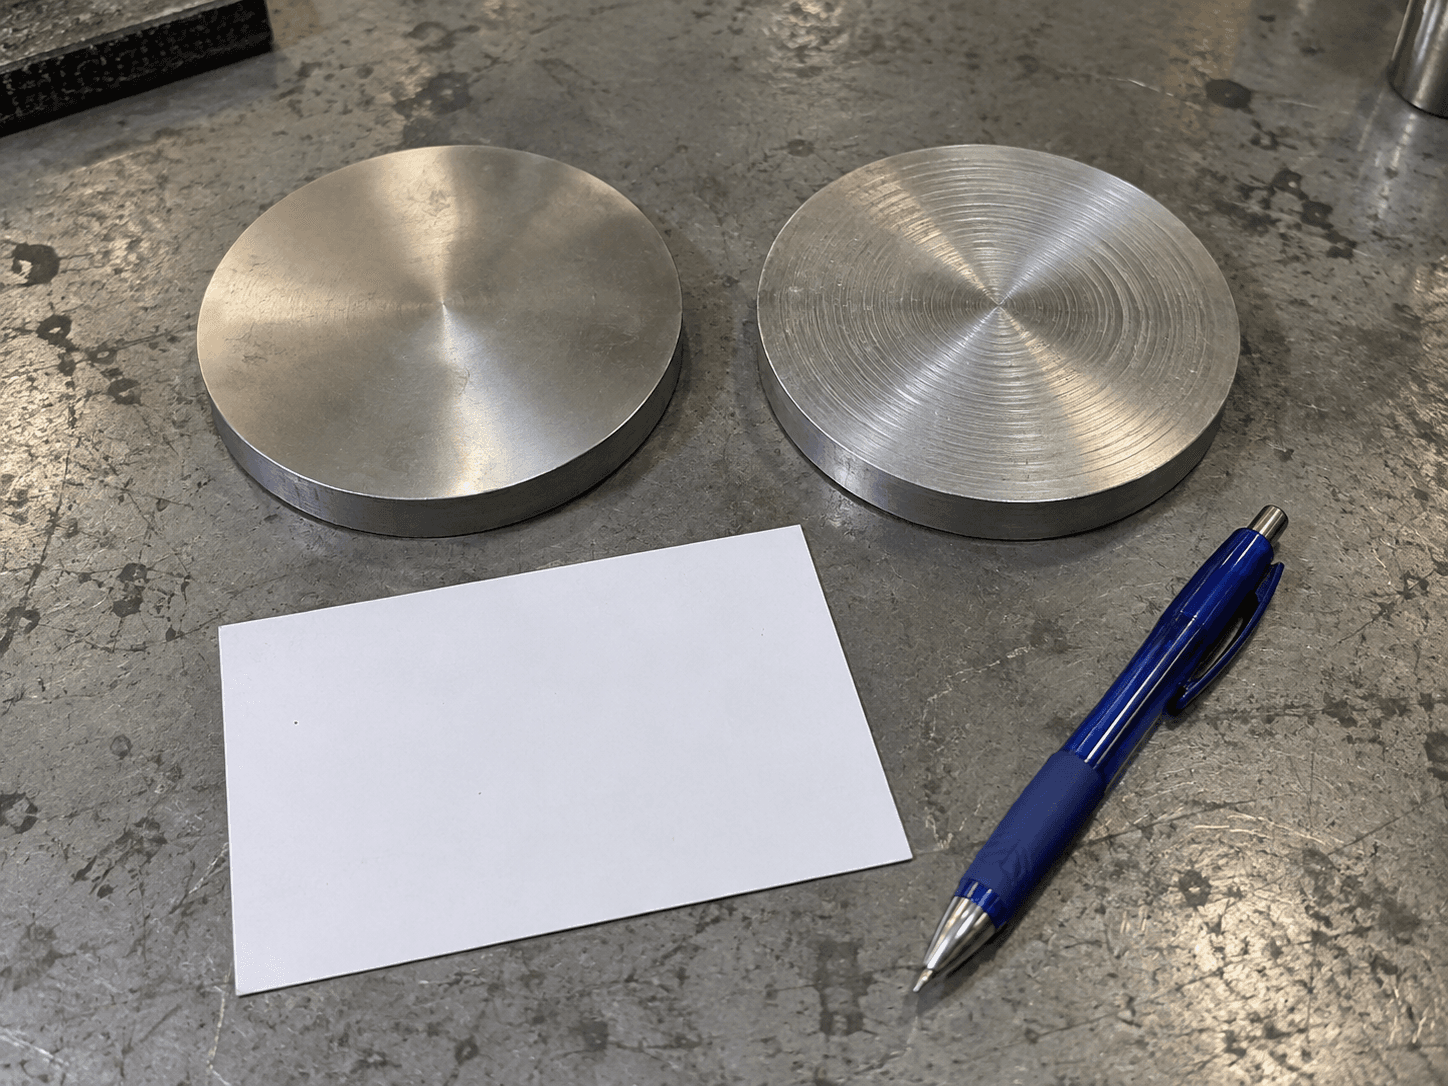
Does a Shiny Part Meet Its Surface-Roughness Requirement?
Separate appearance from measured roughness before choosing a finishing process. Agree on the surface, inspection method and other features that must pass.
Read →
How Do You Repeat a Good Mass-Finishing Result on the Next Shift?
A timer setting is not a process record. Capture the part, setup, consumables and acceptance checks before handing a finishing job to the next shift.
Read →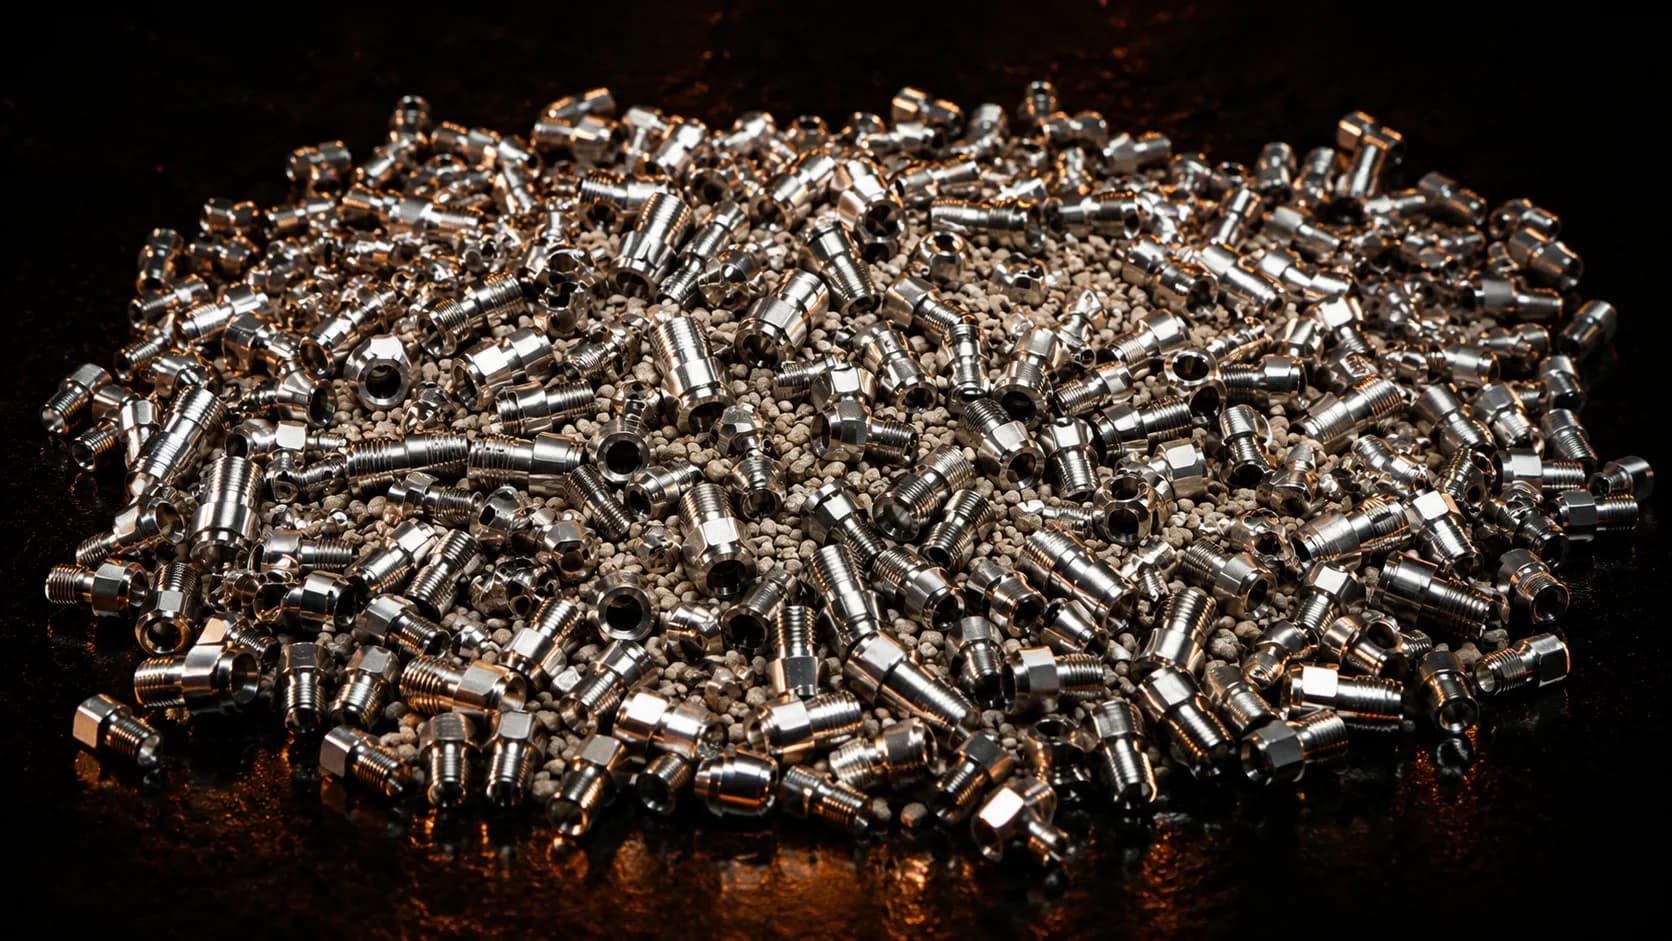
Deburring Firearms Magazines and Ammunition Components with Centrifugal Barrel Finishing
Feed lips, followers, floor plates, and guide rails need a burr-free edge on every unit or the magazine fails under fire. Centrifugal barrel finishing gives the same isotropic edge on the ten thousandth part as the first. Here is how the process is set up.
Read →
Hand Deburring vs Centrifugal Barrel Finishing: What a Shift on the Bench Really Costs
One operator hand deburring for a shift costs roughly $60,000 a year in labor alone, and the edge still varies part to part. A centrifugal barrel finishes the same batch in about 30 minutes with the same edge every time. Here is the honest comparison.
Read →
Case Study: Matching Hand-Polish Quality on Aerospace Parts, Repeatably
A Tier 2 aerospace shop doubted a barrel could match hand polishing. The isotropic finish came back even on every edge and bore, and it came back the same way every batch.
Read →